

Best Quality Checks for Castings That Matter
A casting can look sound on the pallet and still fail once it reaches assembly, pressure testing or field service. For buyers of brass, bronze and copper alloy components, the best quality checks for castings are those that confirm the properties that affect real performance: correct material, controlled dimensions, sound internal structure and reliable sealing surfaces. Inspection must be matched to the part’s function, not treated as a final-stage formality.
Best quality checks for castings start with the specification
Quality control is only meaningful when the acceptance criteria are clear. Before production begins, the drawing and purchase specification should define the alloy grade, critical dimensions, machining allowances, thread requirements, pressure duty, surface finish and permitted defects. For OEM castings, it should also identify datum points, areas that will be machined and any cosmetic requirements.
This matters because not every visible mark is a reject, and not every apparently clean casting is acceptable. A minor mark outside a functional area may have no effect on service life. Porosity near a threaded port, valve seat or pressure boundary is a different risk entirely. A supplier should understand this distinction before setting inspection methods and sampling levels.
Verify alloy chemistry before parts move forward
The first major control is material verification. Brass and bronze castings rely on closely managed alloy composition to achieve the required strength, machinability, corrosion resistance and pressure performance. A material mix-up can create problems that are not visible until machining or service.
Chemical analysis is normally carried out using calibrated spectrometry or another suitable material-identification method. Results should be compared with the specified alloy range, including key elements that influence performance. For example, lead content, zinc level and tin content may all be critical depending on the component, its application and the applicable customer or regulatory requirements.
Material traceability should connect the finished batch to its melt record. That record should identify the alloy, furnace or melt number, date and relevant test result. For high-volume production, this provides a practical route to containment if an issue is found later. It also gives procurement teams confidence that repeat orders are being produced to the same controlled material standard.
Check dimensions at the casting and machining stages
Dimensional inspection prevents one of the most expensive forms of casting failure: a component that cannot be machined, assembled or sealed correctly. The right approach is to inspect dimensions in stages rather than waiting until the final operation.
At the as-cast stage, checks should confirm overall envelope size, wall thickness where practical, core location, casting weight and machining allowance. These controls identify shift, distortion, incomplete fill and excess stock before unnecessary machining time is added.
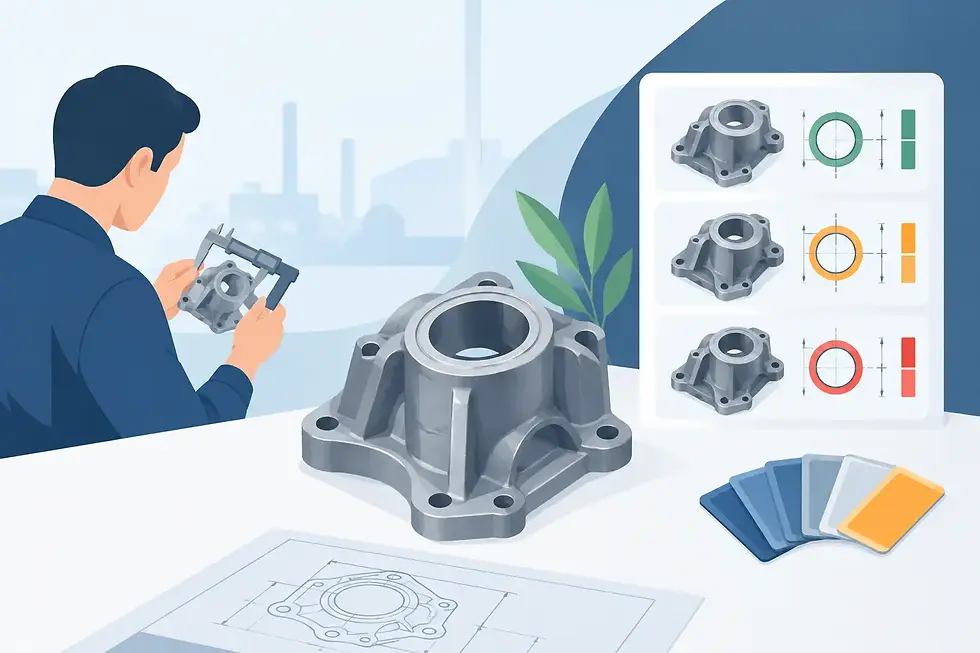
After machining, inspection should focus on the features that determine fit and function. These commonly include bore diameters, flange faces, sealing lands, thread forms, port positions, concentricity and datum-to-datum relationships. Vernier callipers and gauges may be sufficient for straightforward dimensions, but critical features may require go/no-go gauges, bore gauges, height gauges or coordinate measuring equipment.
The most useful inspection plan separates critical dimensions from general dimensions. Applying the same frequency to every feature increases cost without necessarily improving quality. A valve body sealing face and a non-functional external profile do not carry the same risk, so they should not receive the same level of control.
Inspect surface condition with function in mind
Visual inspection remains one of the best value quality checks for castings when it is performed by trained inspectors against agreed standards. It identifies obvious issues such as cold shuts, misruns, flash, sand inclusions, cracks, excessive roughness and damage from handling.
However, visual inspection should never be the only gate. Some defects are superficial and can be removed during machining or finishing. Others can signal deeper problems. A dark line around a junction, for instance, may be harmless surface staining or evidence of a cold shut that compromises strength. Clear acceptance samples, photographs and defect classifications help inspectors make consistent decisions across shifts and batches.
Particular attention should be paid to sealing faces, thread entries, thin walls, sharp transitions and areas around gates and risers. These locations are more likely to reveal issues caused by filling, solidification or trimming.
Use non-destructive testing where the risk justifies it
Non-destructive testing, or NDT, provides evidence about defects that visual checks cannot reliably detect. It is particularly relevant for safety-related, pressure-containing or highly loaded components. The appropriate method depends on alloy, geometry, wall thickness, production volume and the consequence of failure.
Common options include:
Dye penetrant testing for surface-breaking cracks and discontinuities on non-porous surfaces.
Radiographic inspection for internal shrinkage, inclusions and voids in selected areas.
Ultrasonic testing for internal discontinuities in suitable sections and geometries.
Magnetic particle testing for ferrous castings, though it is not applicable to brass and bronze.
Leak or pressure testing for components designed to contain fluids or gases.
NDT is not automatically required on every casting. Full radiography of a simple low-pressure fitting may add cost and lead time with little practical benefit. Conversely, relying on appearance alone for a pressure-critical valve body is a false economy. The inspection method should be selected through a risk-based discussion between the buyer and manufacturer.
Pressure-test components that must seal
For valve bodies, pump parts, hose fittings and water-handling components, pressure testing is often the decisive functional check. It confirms whether porosity, cracks or machining defects create a leak path through the pressure boundary.
The test medium, pressure level, hold time and acceptance criteria must be agreed in advance. Hydrostatic testing is commonly preferred where appropriate because water stores less energy than compressed air. Pneumatic testing may be used where the application requires it, but it demands careful safety controls.
A passed pressure test does not replace dimensional or material verification. A component can be leak-tight yet made from the wrong alloy, or it can pass at one pressure but lack sufficient wall thickness for the intended duty. Used alongside the other controls, however, pressure testing provides direct evidence of service suitability.
Control the process, not only the finished part
Final inspection catches defects, but process control reduces their occurrence. Foundry quality depends on disciplined control of mould preparation, core quality, melt temperature, pouring practice, cooling time, fettling and heat treatment where specified. Variability at any of these stages can affect dimensions, porosity and mechanical properties.
For repeat components, a capable supplier records key production parameters and reviews defect trends by batch. If porosity rises in a particular feature, the response should go beyond sorting the finished parts. The team should investigate gating, feeding, venting, melt practice or core position and then verify that the corrective action has worked.
This approach is especially valuable for offshore supply programmes. The practical benefit is not simply a certificate at dispatch. It is consistent production from one order to the next, fewer disruptions at the buyer’s facility and less need for expensive incoming sorting.
Set sampling levels that reflect the application
Inspection sampling should be proportionate to risk. Low-risk, high-volume catalogue items may be controlled through defined batch sampling, first-off inspection and regular process checks. Custom parts with tight tolerances, pressure duty or a new tooling design may require enhanced first-article approval and more frequent dimensional verification.
The key is to define what happens when a sample fails. A clear containment process may require expansion of the sample, segregation of the lot, review of records and corrective action before release. Without this discipline, sampling can become a paperwork exercise rather than a genuine protection for the buyer.
At Tan Tasa UK, casting quality is considered alongside machining, assembly requirements and the final operating environment. This supports a more practical inspection plan for standard components and OEM parts alike, without adding unnecessary cost to every order.
Ask suppliers for evidence, not broad assurances
When comparing casting suppliers, buyers should ask how material is verified, which dimensions are inspected, whether pressure testing is available, how batches are traced and what records can be supplied with the shipment. The answers should be specific to the component, not a generic statement that all products are checked.
A dependable supplier will also be candid about trade-offs. Tighter tolerances may require additional machining. More extensive NDT may affect unit cost and lead time. A revised casting design may reduce porosity risk but require tooling changes. These are commercial and engineering decisions best made early, when they can improve both cost and reliability.
The strongest quality programme is one that gives buyers useful evidence before parts enter their production line. When checks are linked to the actual failure risks of the casting, quality control becomes a practical safeguard for performance, delivery and total procurement cost.


Comments